
One of the most common questions from laboratories considering laser diffraction is: "Which dispersion method is best suited to my sample?" We welcome this question because it opens a broader discussion about the goals of the measurement, the nature of the sample, and the workflow requirements of the laboratory.
In this application note, we discuss why both wet and dry dispersion options exist, how they differ, and the key considerations that can help determine which approach is best suited to your materials, particle sizing requirements, and measurement goals.
With the Mastersizer 3000+ range, samples can be dispersed either in a liquid or in air. This does not require two separate instruments. The same optical bench, which houses the light source(s) and detectors, can be configured with either wet or dry dispersion accessories. This flexibility allows laboratories to switch between dispersion methods as required, whilst the easily interchangeable measurement cells ensure accurate optical alignment without the need for tools or manual realignment.
In the wet dispersion configuration, several dispersion units are available that vary in both dispersion volume and level of automation. This flexibility is important because different applications have very different sample requirements. Some applications only have small quantities of sample available, meaning that excessive dilution in a large-volume system could lead to poor signal-to-noise ratios. In contrast, applications such as soils and sediments often contain coarse, highly polydisperse particle size distributions that require larger quantities of sample to achieve representative sampling. If the dispersion volume were too small for these materials, obscuration could become excessively high, increasing the risk of multiple scattering.
The dry dispersion configuration is equally adaptable. Two base units are available: the automated Aero S and the manually operated Aero M. Additional customization is achieved through the selection of sample feeding trays and venturis. Sample quantity requirements can vary significantly, from precious materials analyzed using a micro-tray to large sample volumes continuously fed from a funnel feeder. Similarly, venturi options differ in their geometry and dispersion energy. High-energy venturis are available for strongly agglomerated materials, while ceramic-lined venturis are recommended for abrasive samples that may cause excessive wear.
Choosing between wet and dry dispersion can initially seem daunting, but a few key questions can help identify the most suitable approach as shown in Figure 1.
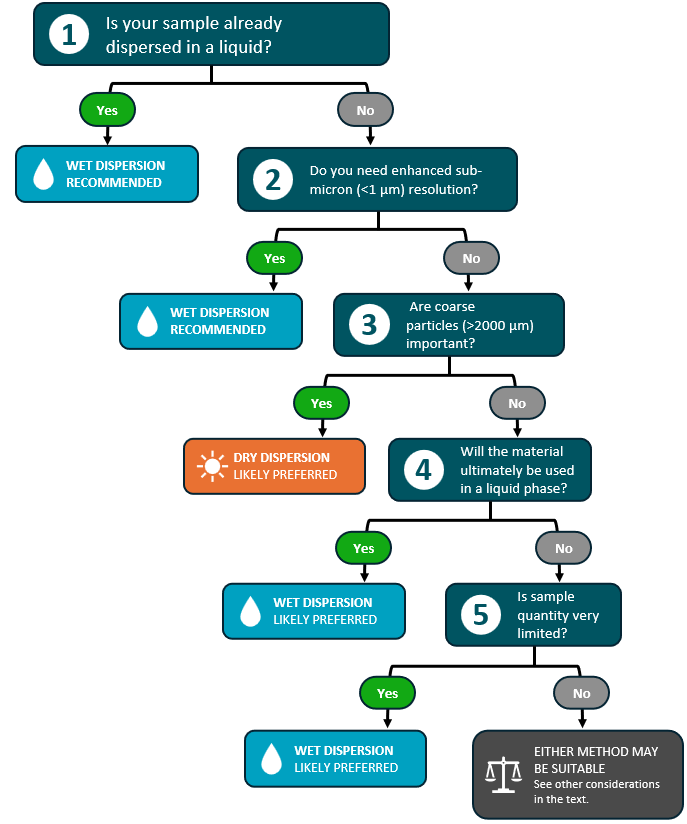
Figure 1: Decision making flowchart to help determine the best dispersion mechanism. This is just a preliminary guide. Many materials can be measured successfully using either wet or dry dispersion. See the main text for more details and further considerations.
It is important to remember that there is rarely a universally correct answer. In many cases, both approaches can successfully measure the same material, meaning the final decision may be influenced by practical considerations as much as by particle sizing performance.
One of the most important considerations is the particle size range you need to measure. A significant difference between wet and dry dispersion is the minimum particle size that can be measured with confidence. Using wet dispersion, the Mastersizer 3000+ Ultra incorporates a secondary blue LED light source, enabling sizing measurements down to 0.01 µm. Therefore, if characterization of submicron particles is important, wet dispersion on the Mastersizer 3000+ Ultra is typically the preferred approach.
As particle size decreases, the surface area-to-mass ratio increases, making attractive Van der Waals forces increasingly significant. As a result, additional dispersion energy is often required to break apart agglomerates and reveal the true particle size distribution. While many fine materials (<10 µm) can be dispersed successfully using compressed air and the inherent particle-particle collisions in a dry system, some materials require higher dispersion energy, such as ultrasound or chemical stabilization with surfactants or additives, which is only available in wet dispersion. For applications dominated by fine particles, wet dispersion is therefore often advantageous.
At the opposite end of the size range, the Mastersizer 3000+ Ultra with dry dispersion can measure particles up to 3500 µm. This capability is enabled by the larger window spacing within the dry cell and the detector configuration used in the Ultra model. In addition, representative sampling of coarse particles is often easier to achieve in dry dispersion because larger sample volumes can be analyzed during each measurement. Consequently, users primarily interested in larger particle sizes may find dry dispersion more attractive.
If your samples are already suspended in a liquid, wet dispersion is generally the most appropriate choice. For example, suspensions of solid particles in liquids can be diluted into a compatible dispersant before analysis. The same principle applies to emulsions and semisolids, which also necessitate wet measurement methods.
An often-overlooked consideration is whether the measured particle size distribution should reflect the material as supplied or the material as used. For example, a dry graphite powder may ultimately be dispersed in a liquid and subjected to ultrasonic treatment before its final use. In this case, wet dispersion may provide a more representative understanding of the particle size distribution present in the application. Conversely, if a powder will always remain dry throughout its lifecycle, dry dispersion may be the more relevant measurement technique. Aligning the measurement method with the material's end-use environment can often provide a more meaningful understanding of particle behavior and performance.
Both wet and dry dispersion methods can operate with relatively small sample quantities, often in the milligram range. However, the lowest sample consumption is generally achieved with wet dispersion, particularly when using small-volume accessories such as the Hydro SV.
Method development requirements should also be considered. Developing a robust dry dispersion method often requires exploration of multiple feed rates and dispersion pressures, which can consume a significant amount of material. In contrast, wet method development is often less sample intensive. As a result, applications where sample volumes are especially limited frequently favor wet dispersion systems. If sample availability is not a concern, both wet and dry dispersion remain viable options.
Practical considerations surrounding sample handling and waste disposal can also influence the decision. For example, if long-term storage of the material in its dry state is not desirable, dry dispersion may become less attractive because waste powder collected in the vacuum system must be periodically removed and managed. Similarly, materials that pose dust generation or inhalation hazards require careful consideration. Although the Aero dry dispersion units minimize operator exposure during analysis, some exposure will still occur during sample loading and waste disposal meaning that additional safety precautions would be needed.
Conversely, wet dispersion may introduce a liquid waste stream that requires management, particularly when non-aqueous dispersants are needed. The choice of dispersant can also determine whether wet measurement is practical. For example, table salt cannot be measured in water because it dissolves, meaning an alternative dispersant such as isopropyl alcohol (IPA) would be required. However, this introduces additional costs associated with solvent purchase, handling, disposal, and routine cleaning procedures. In such situations, dry dispersion may provide a faster and lower-cost alternative.
For some applications, the considerations discussed above may still leave both wet and dry dispersion as viable options. In these situations, external factors may become the deciding criteria. Many organizations prefer to align methods across multiple sites to improve data comparability and facilitate method transfer. Similarly, industry standards and regulatory guidance documents may recommend particular dispersion approaches for certain materials. Where standards exist, following established methodologies can simplify compliance and improve confidence when comparing results with historical datasets or measurements generated by other laboratories.
As discussed above, there are many materials for which both wet and dry dispersion provide excellent particle size measurements. In these situations, the final decision often comes down to practical considerations such as throughput, operating costs, sample availability, and laboratory workflow.
In the following examples, we will explore several scenarios where both wet and dry dispersion can be successfully applied:
Some materials can be measured equally well using either wet or dry dispersion, producing highly comparable particle size distributions. In these situations, such as the sample shown in Figure 2, the decision between measurement methods is often driven by practical considerations such as throughput, sample availability, solvent handling, and laboratory workflow rather than differences in the particle size results themselves.
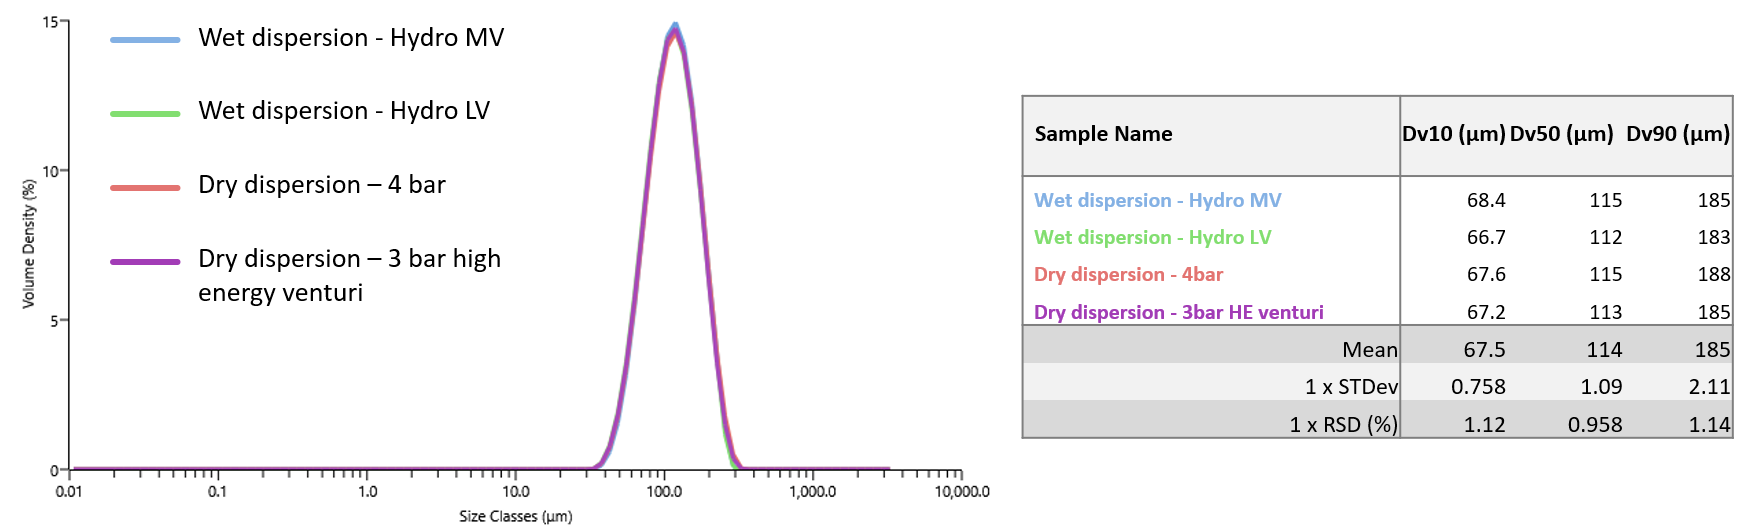
Figure 2: Example of excellent agreement between wet and dry dispersion measurements. Comparable PSDs were obtained across multiple wet and dry dispersion configurations, demonstrating that the measured particle size distribution is robust to the choice of dispersion mechanism.
For some materials, wet and dry dispersion can produce substantially different particle size distributions because they represent different physical states of the material. Yeast is a good example, where wet dispersion can measure the size of individual yeast cells, while dry dispersion may reflect the size of the granules formed during powder processing (Fig. 3). In cases such as these, neither measurement is inherently more correct; instead, the appropriate method depends on whether the user is interested in the material's behavior in a wet process or as a dry powder.
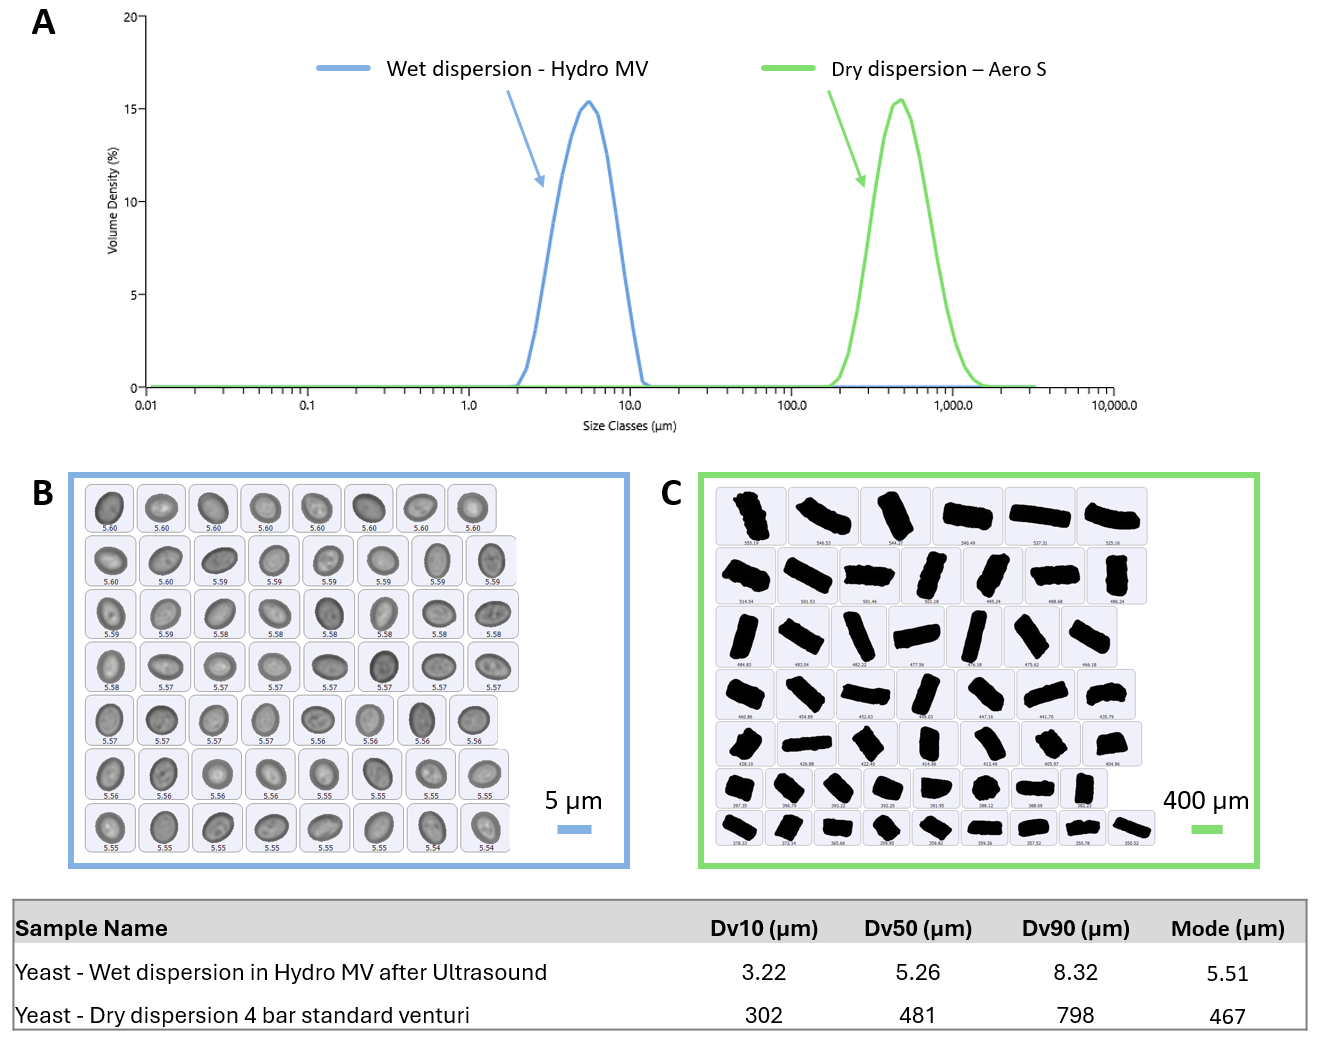
Figure 3: Example of a material where wet and dry dispersion provide different, but equally meaningful, particle size distributions. Wet dispersion with ultrasound measures the size of individual yeast cells after deagglomeration, while dry dispersion characterizes the size of the coarse granules. A) Mastersizer wet and dry particle size distributions. B) Morphologi 4 thumbnail images of modal particle size of yeast cells (wet dispersion). C) Morphologi 4 thumbnail images of modal particle size of yeast granules.
Wet and dry dispersion should not always be viewed as competing techniques. In some applications, they can provide complementary information about the material. Comparing results obtained using both methods can provide valuable insights into agglomeration behavior, particle strength, dispersion mechanisms, and susceptibility to breakage. Used together, wet and dry dispersion can act as orthogonal techniques that help build a more complete understanding of particle behavior than either approach alone (Fig. 4).
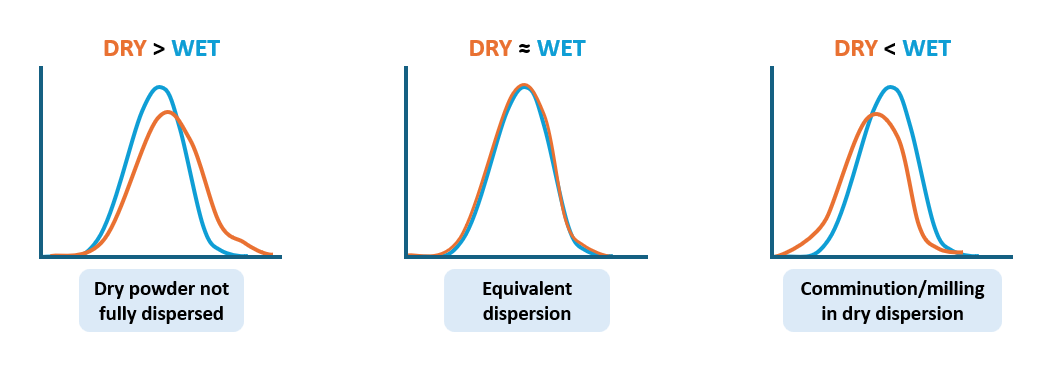
Figure 4: Graphic demonstrating how wet and dry dispersion results can provide valuable insight into particle behavior. Coarser dry results indicate incomplete deagglomeration, while finer dry results may suggest particle breakage during dispersion. Agreement between wet and dry measurements provides confidence that both methods are characterizing the particles in a similar state of dispersion.
Both wet and dry dispersion can provide accurate and reproducible particle size measurements on the Mastersizer 3000+. The most appropriate choice depends on a combination of factors, including particle size range, sample availability, end-use conditions, sample handling requirements, and any relevant industry standards.
While some materials clearly favor one approach, many can be measured successfully using either method. In these cases, practical workflow considerations often become the deciding factor, and comparative testing can provide valuable additional insight into material behavior.
If you are unsure which approach is most suitable for your application, please get in touch. Discussing your requirements with an applications specialist can often help identify the most efficient solution. Proof-of-concept testing can also provide valuable evidence to support instrument and accessory selection.